
In the textile testing lab, ISO 105 X12 is a popular test. Customers have specific testing protocols and requirements, as well as criteria of Pass and Fail for various fabric properties. If you are a technician in a textile lab, this article focusing on the Color Fastness to Rubbing test ISO 105 X12 method may be helpful for you.
In modern textile testing laboratories, ISO 105 X12 is used as a standardized benchmark to evaluate surface dye adhesion under frictional forces. With the help of this testing method, we can optimize processes during dyeing, printing, and finishing operations, ensuring the reproducibility of results worldwide. A person who can understand this method can diagnose dye-fiber bonding issues, optimize curing parameters, and prevent the rejection of customer dye to poor-quality crocking grades.
Why Color Fastness Testing is Important
Color fastness is a very important factor for textile materials, including towels, bedding, apparel, and garments. The color of any dyed or printed article must be strong enough not to transfer from the surface of the fabric to another material. To achieve the best color fastness, a special selection of dyes or pigments is required. This ensures that the colors remain vibrant and do not fade or bleed, maintaining the quality and durability of the textile products. Proper testing and selection of materials are essential to meet the high standards of color fastness in the textile industry. Crocking or rubbing is a common issue in textiles.
From a technical point of view, colorfastness represents the efficiency of chemical fixation on the dye molecules within the fiber matrix. Reactive dye forms a covalent bond with the cotton fibers, and disperse dyes diffuse into the amorphous zone of polyester.
What is Color Fastness to Rubbing?
Color fastness to Rubbing means when fabric touches or contacts with another surface by friction or rubbing, if the fabric bleeds color on another surface or self-stains, we need to test the rate of color fastness to rubbing. It is also known as colorfastness to crocking.
There are two common methods of Rubbing. One is the American (AATCC 8) method, and the other is the ISO method. This article is about the ISO standard of rubbing: ISO 105 X12.
Rubbing fastness test simulates the stress of abrasion, a fabric faces during wear, laundering, or handling. Fibers with protruding ends, high hairiness & rough texture, such as open-end cotton yarn or regenerated cellulose such as viscose, exhibit lower rubbing fastness due to enhanced surface fractional area and potential of dye migration.
What is the ISO standard for color fastness to rubbing?
ISO (International Organization for Standardization) has a series of standards for testing various color fastness, like color fastness to washing, color fastness to water, perspiration, color fastness to light, and many more. For color fastness to rubbing test ISO 105 X12, it includes the type of rubbing action, pressure applied, and assessment of the color transferred onto the standard fabric.
ISO 105 X12 emphasizes the controlled testing conditions to decrease the operator bias. Different parameters, such as pressure (9 ± 0.1 N), rubbing track length (104 mm), and cycle count, are fixed to maintain global comparability. Calibration of the Crock Meter and conditioning of the test specimen under 21 ± 2 °C and 65 ± 5 % RH are very necessary to achieve accuracy.
What is ISO 105 X12
The international testing method ISO 105-X12 is performed to evaluate the rating of color transfer from dyed or printed textile articles to the surface of other materials, whether colored, printed, or white. This method provides guidance to recheck our processes and make necessary adjustments to the dye recipes or auxiliaries used. By following ISO 105-X12, we can ensure better color fastness and improve the quality and durability of textile products, reducing the risk of color transfer and maintaining customer satisfaction. ISO 105-X12 is a method in which both dry and wet tests are performed using a DaRong crock meter and an adjacent referenced white fabric. The color fastness is evaluated with the help of a grey scale. This method helps determine the resistance of the fabric’s color to rubbing off onto other materials, ensuring the quality and durability of textile products. ISO 105 X12 includes the type of rubbing action, pressure applied, and assessment of the color transferred onto the standard fabric.
Dry rubbing evaluates the mechanical anchorage of dyes and pigments while wet rubbing evaluates the dye solubility and the effect of moisture on color transfer. Due to the analyzation of both dry and wet conditions, we get a complete understanding of surface color stability.
Purpose of Colorfastness to Rubbing Test
1. Fabric will not Bleed or transfer color onto other fabric or surfaces.
2. Fabric will not Fade excessively due to friction or abrasion.
3. Fabric will not cause staining or discoloration of adjacent material.
The results of this test also assist R&D and QA departments to determine preferred curing temperature, selection of binder and dye fixation percentage. This test is acts as diagnostic tool to detect insufficient soaping, migration during stenter drying. ISO 105 X12 is not only a quality control test but also a process-optimization indicator.
Textile Testing Equipment and Tools for ISO 105 X12
In Textile Laboratories, for IS0 105 x12, we need an automatic rubbing fastness tester with a specific weight on the rubbing finger (9 ± 0.1 Newton) and a length of path 104 mm. Rubbing finger diameter 16 ± 0.3 mm. 10 cycles per second.
Rubbing cloth recommended by ISO 105 F09 (5×5 cm square, 100% cotton bleached)
For assessment by Grey Scale ISO 105 A03, Light source D – 65 is recommended.
- Rubbing Cloth specification: Rubbing cloth must be Cotton and De-sized, bleached without finish fabric, size of the rubbing cloth must be 50 ± 2mm square.
- Conditioning: Four hours.
- Soft-back waterproof abrasive paper or grating of stainless steel wire 1mm in diameter and mesh width about 20mm.
- Rub to and fro in a straight line, 10 times to and 10 times fro. along the truck (104 ± 3 mm long).
DaRong Crock Meter
- Rubbing figure size = 16 mm
- Rubbing track length =104 3 mm
- Downward force= 92 N
- Required cycles =10
- Weighing balance
- Rubbing cloth should be pretreated such as desized, bleached and size should be 50 mm.
- Filter paper to absorb extra water in wet rubbing.
- Weighing balance
- Drooper
- Distilled water
- Gray scale to evaluate results.
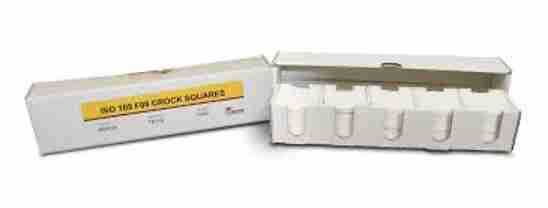
 Crocking Clothes

 Crock Meter
There should be include verification of downward force in equipment calibration by using a certified balance and stroke length using a precision scale. The rubbing cloth must be replaced after each and every test to prevent contamination. Due to high absorbency and neutral color, cotton rubbing fingers are selected to enable accurate visual assessment on the gray scale for staining. For wet rubbing, distilled water should be used to ensure uniform wetting without any residual contamination.
Insight and Experience on Test Method ISO 105 x12
Preparation of the testing specimen
Cut six dyed or printed specimens having a size of 50mm x 140 mm for both dry and wet rubbing.
If the specimen is a yarn or thread, then it knits at least 50mmx140 mm
Keep the crocking cloth and testing specimen for 4 hours in a standard atmosphere having 21 2 degrees centigrade temperature and 655 degrees relative humidity.
Testing must be performed under a standard atmosphere to achieve the best results.
Lab technicians should ensure that the testing specimen represents the actual production batch and includes all finishing treatments, such as softener, coating, or resins that can alter surface friction.
ISO 105 X12 Test Method Procedure
DaRong crock meter is already ready to use, and no need for any external metal wire.
Dry Rubbing
As a lab technician, for testing, you will need to:
- lay the Sample on abrasive paper
- fix the Rubbing cloth on rubbing machine finger and put on fabric.
- Avoid using selvage of fabric
- Press the starting button and observe the to and fro motion without touching anything other.
- When the machine stops, take out the Rubbing cloth and keep it in air-dry condition.
- Asses the rubbing cloth by using a grey scale of Staining ISO 105-A03 under suitable D-65 light.
- Rubbing should be done in both directions: warp and weft direction.
Wet Rubbing:
- Lay the sample on abrasive paper.
- Weight the Conditioned rubbing cloth, then soak in Distilled water by drop or soak by petri dish and reweight to get the pick up 95% to 100% with the help of blotting paper.
- Fix the Rubbing cloth on the rubbing fastness tester finger and put it on the fabric.
- start the machine and observe the to and fro motion
- After the machine stops, take out the Rubbing cloth and fabric
- Dry the Rubbing cloth in air dry condition.
- Assessment is the same as Dry Rubbing Assessment.
- Rubbing should be done in both directions: warp and weft direction.
While performing the wet rubbing, controlling the moisture pickup between 95-100% is very critical, because oversaturation will cause dripping and non-uniform transfer, while under-wetting will reduce dye mobility. Always perform more than 1 test in both warp and weft directions for reliable data symmetry. Recording testing conditions alongside test results helps correlate unexpected grade deviation with environmental factors.

Interpreting the color fastness results
Interpreting the color fastness results involves understanding the results or rating scales and what they indicate about a fabric’s color performance.

Rating Scale
The rating scale is the measurement of color bleeding on the standard rubbing cloth fabric.
Ratings are poor to good from rating 1 to rating 5 given below:
- Rating 1 is a very poor color fastness property.
- Rating 2 is poor color fastness property.
- Rating 3 is moderate color fastness property.
- Rating 4 is a good color fastness property.
- Rating 5 is excellent color fastness properties like no impact of rubbing.
Results should be evaluated with the help of a grey scale under standard lighting D-65. Lab technicians should use a calibrated lightbox and avoid subjective comparison under ambient or yellow light sources. For most precision control, the spectrophotometer delta E reading should be used to correlate with visual ratings of the numerical color difference values.
Pass/Fail Criteria
Pass or fail criteria are based on customer demand. Mostly, below 3 are called failed by the customer, and 3 or above 3 are mostly acceptable by the customer.
From the behavior of chemicals, low rubbing fastness can stem from incomplete dye fixation, or dye migration during dyeing, excessive residue of surfactants or mechanical abrasion of pigment film.
FAQs
What is the ISO 105 X12 method?
ISO 105-X12 is a globally recognized testing method used to evaluate how much color transfers from a dyed or printed textile to another surface. This method helps ensure that textiles maintain their color integrity and do not bleed onto other materials, maintaining the quality and durability of the products.
Why color bleed or transfer from one surface to another?
In dyed textiles, color bleeding occurs when unfixed dyes are not fully removed during the finishing process. This can lead to dyes transferring from one surface to another. To address this issue, the dyed materials should be hot-washed to ensure all unfixed dyes are completely removed. When dyes are not properly bonded to the fibers, they can easily transfer, causing color bleeding. Proper bonding of dyes to the textile fibers is crucial to prevent this transfer and ensure the color remains stable and does not bleed onto other surfaces. This process helps maintain the quality and appearance of the dyed textile materials.
How can we improve color fastness to rubbing?
There are several methods to improve color fastness to rubbing:
1. Fixer Application: after the dyeing or Printing process, we apply a fixer to improve the color fastness property of the fabric.
2. Dye Selection: it is also a very important technique by which we can save time and maintain customer quality.
3. Washing and finishing: Use good washing and finishing techniques to remove excess dye and fix the color.
4. Heat treatment: Apply heat to fix the dye on the fabric and improve fastness.
What is the difference between ISO and AATCC methods?
1. Rubbing direction: The AATCC method is the diagonally rub of the fabric while the ISO method mentions the direction of warp straight and weft straight, not diagonally.
2. AATCC method recommended in wet rubbing; pick-up should be 65% ± 5 %. ISO recommended pick-up should be 95 % to 100 %.
Related Resources
Crockmeter/Rubbing Colorfastness Tester